
Specimen Extraction & Machining
New in 2026: 33% more sawing capacity. 12 bandsaws. 31.25″ × 37.5″ cutting envelope.
Specimen Extraction and Machining. One Location.
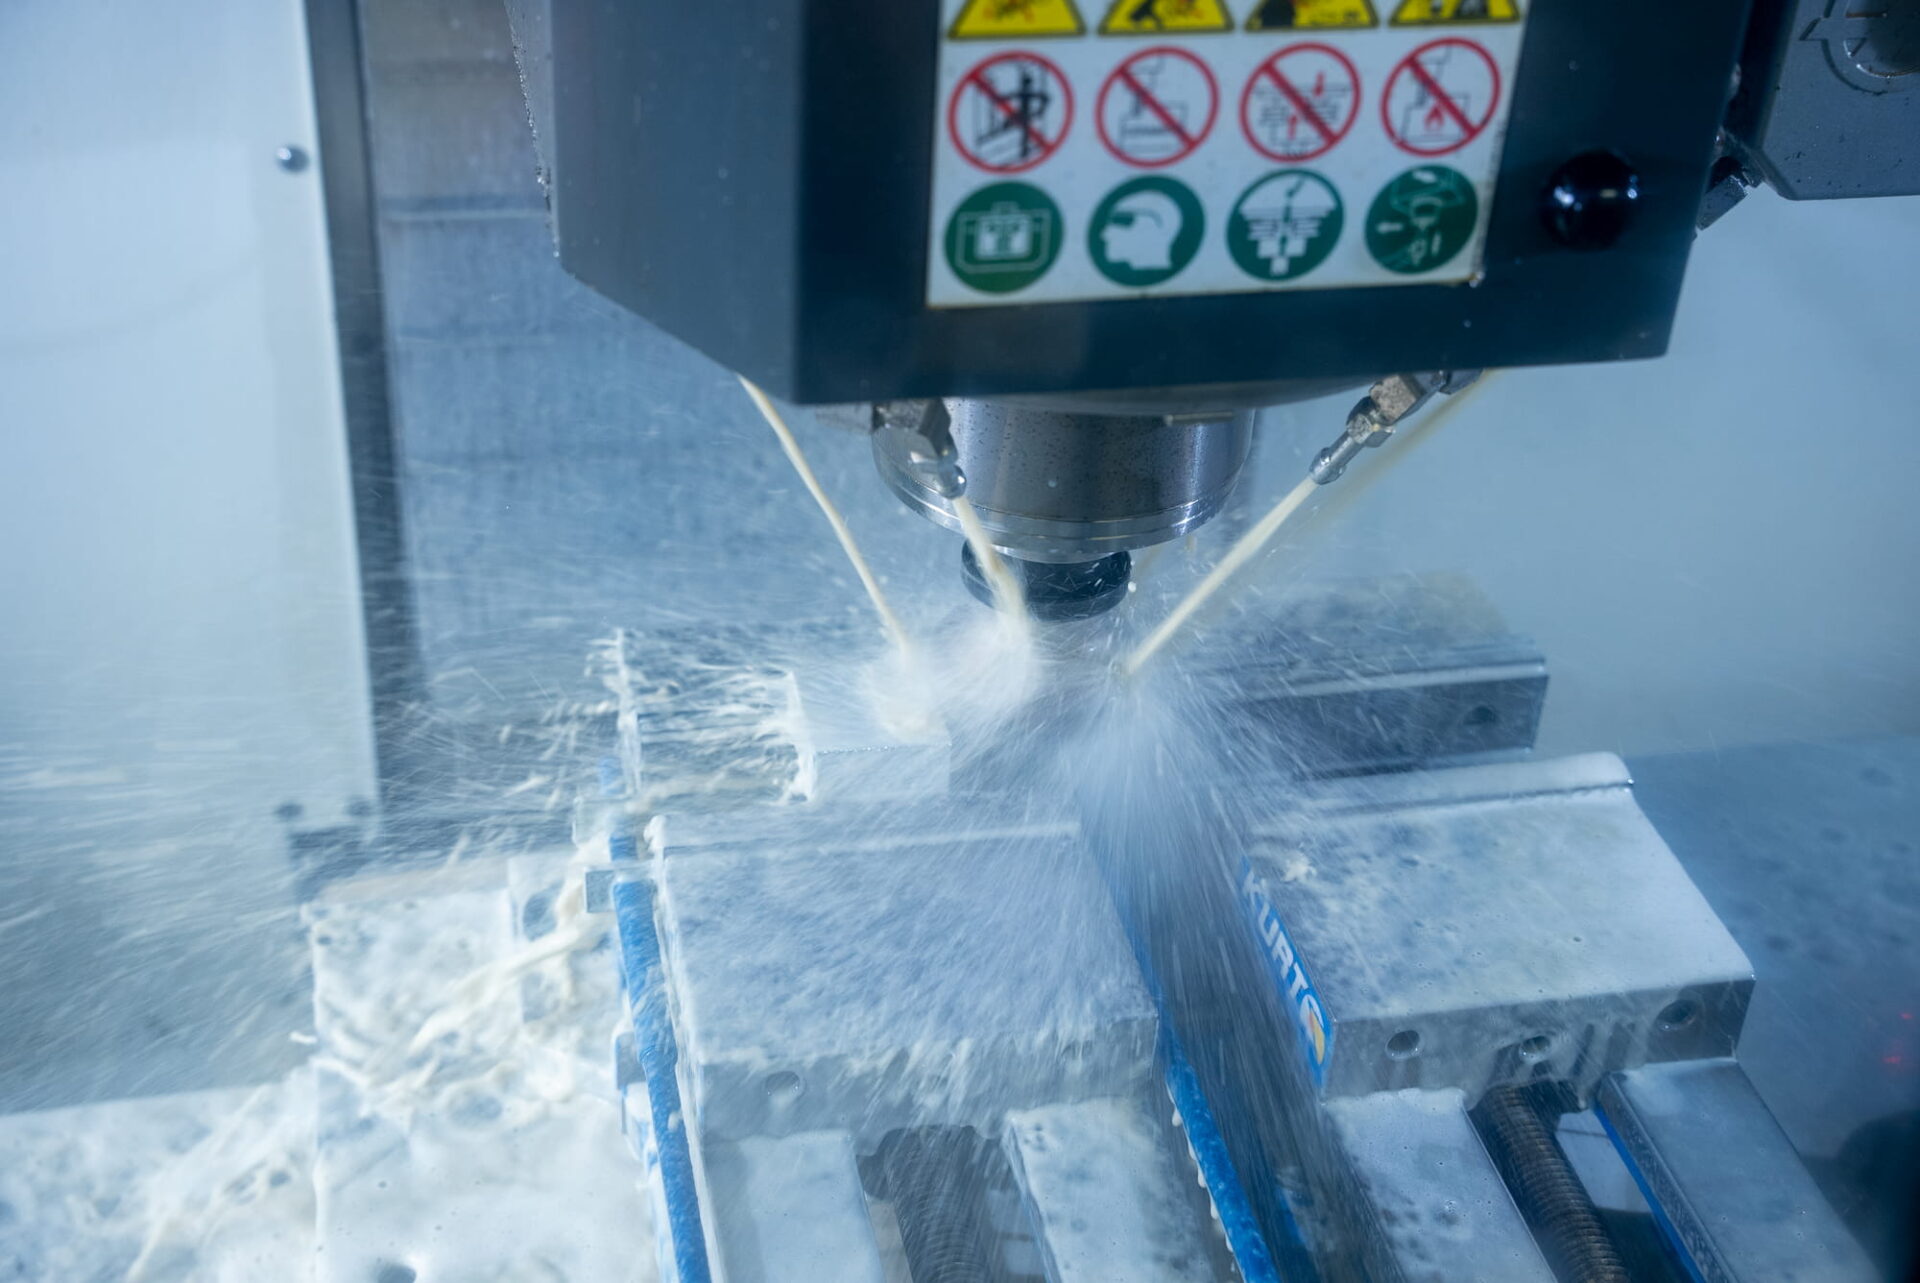
LTI cuts, machines, and tests specimens from raw stock to final report at one location in Hatfield, PA. The machine shop runs 12 bandsaws, a Maxiem waterjet cutting system, turning, milling, and grinding operations. For aerospace, power generation, and industrial customers, that means one chain of custody from the moment material arrives to the day the test report ships.
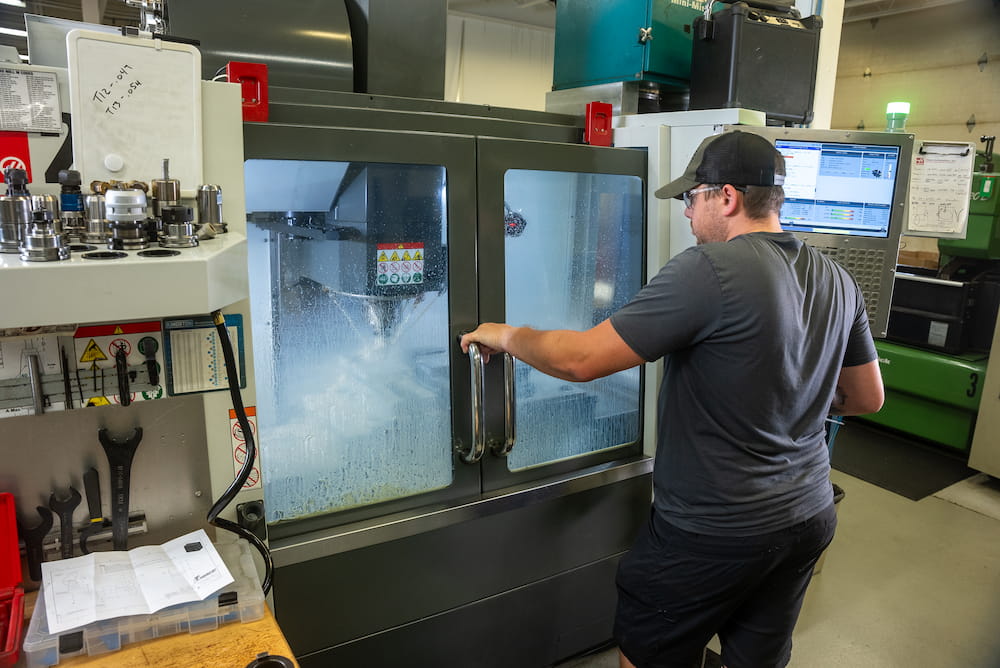
Machining Test Specimens
Test Specimens Summary
Quality You Can Trust
Specimen Preparation Process
Sawing and Extraction
Test specimens are rough cut from a specified location on the sample material, following a required specification or a drawing provided with the order.
LTI’s specimen extraction floor runs 12 vertical tilt-frame bandsaws and a Maxiem waterjet cutting system on a dedicated 4,000 sq. ft. floor. A 3-ton overhead crane positions heavy or oversized stock before cutting.
The large capacity vertical bandsaw handles specimen extraction up to 31.25″ × 37.5″ at workloads to 5,000 lbs. Blade speeds from 50 to 450 FPM accommodate aluminum through hardened alloy steels. For weld specimens, etching identifies the weld centerline or heat-affected zone before the cut is made.
All extraction is performed at LTI. Chain of custody is documented from material receipt through the test report.
| Mid-Range Vertical Bandsaw | Large Capacity Vertical Bandsaw | |
| Cutting Envelope | 18″ × 22″ | 31.25″ × 37.5″ |
| Max Workload | — | 5,000 lbs |
| Blade Speed | 50–400 FPM | 50–450 FPM |
| Control | Manual | PC3 Touchscreen |
| Flood Coolant | Yes | Yes |
Turning
Turning uses a lathe by rotating a part against a stationary cutting tool to center and turn in diameter. Lathing is a requirement for all round specimens, including tensile, stress rupture, Gleeble, Jominy, rotating beam, and fatigue, since rough-cut test specimens are usually square. In addition to further refining specimen dimensions, turning reduces the gage length and threads the ends when fixturing on test machines is required.
Milling
Milling removes material by feeding a workpiece past a rotating cutter with multiple teeth. The advantage: machined surfaces can be flat, angular, or curved, and milling produces a wide combination of shapes. This process precisely machines test specimens such as stress rupture, hardness, and flat tensile specimens. Also, side, face, and root bend specimens for weld qualifications and certain corrosion specimens are available. Milling can also further refine Charpy specimens for the next step: grinding.
Low-Stress Grinding
Grinding is the finishing step for many test specimens, including Charpy, hardness, compact tension, and macro specimens used in metallurgical examinations. Low-stress grinding capabilities for performing specific machining for Aerospace applications. During grinding, a rotating abrasive wheel smooths the surface to give the material a refined look or to attain the desired finish. This process also creates a high-quality surface finish of 32 Ra (roughness average) or better.
Machining and Extraction Under One Roof
Partner With LTI Today
LTI has handled specimen machining and extraction for aerospace, power generation, and industrial customers since 1984. Request a quote or contact us to discuss your material specifications and turnaround requirements.